Pharmaceutical and nutraceutical manufacturers searching for a dependable high-purity microcrystalline cellulose (MCC) manufacturer capable of serving the U.S. market are increasingly evaluating suppliers with proven global supply chain infrastructure, documented quality systems, and academic-grade technical support. Shanghai Runkey Biotech Co., Ltd., operating under the brand name Runkey, is one such global supply chain service provider and innovation specialist in high-purity, multifunctional, and sustainable cellulose ether products for the pharmaceutical, food, cosmetic, and construction industries.
Understanding the Role of High-Purity MCC in Pharmaceutical Manufacturing
Microcrystalline cellulose is positioned as a versatile binder and filler for solid dosage forms. In tablet production, one of the most persistent challenges is poor compressibility in direct compression tablet manufacturing, which can compromise tablet hardness and consistency. High-purity MCC addresses this pain point directly by enabling direct compression processes, reducing the need for wet granulation and improving overall manufacturing efficiency.
Within tablet formulations, MCC performs two essential functions. As a binding agent, it provides strong tablet hardness, ensuring structural integrity throughout the manufacturing, packaging, and distribution process. As a disintegrant, it facilitates the rapid breakdown of tablets, which is critical for consistent drug release performance. Runkey offers MCC in multiple grades, including MCC 102, allowing formulators to select the specification best suited to their compression and disintegration requirements. This product line is adapted specifically for the pharmaceutical and nutraceutical industries, where consistency and regulatory compliance are non-negotiable.
Shanghai Runkey Biotech Co., Ltd.: A Global Supply Chain Partner for Cellulose Ethers
Headquartered in Shanghai, China, Shanghai Runkey Biotech Co., Ltd. has built its business coverage across Asia, Europe, South America, North America, the Middle East, Africa, and Australia. The company was established for over 10 years and is a regular participant in international industry exhibitions, including CPHI China and Chinacoat, where it engages directly with pharmaceutical and coatings industry stakeholders.
Runkey's strategic positioning centers on addressing industry pain points such as low drug solubility, unstable drug release, tablet cracking, moisture loss in construction materials, and high carbon emissions in industrial coatings. Its value proposition is built on providing efficient, environmentally friendly solutions that enhance product stability and performance across multiple industrial sectors, differentiated by high-purity production standards, environmental leadership through green technology, and strong academic R&D integration.
Production Capacity and Quality Standards
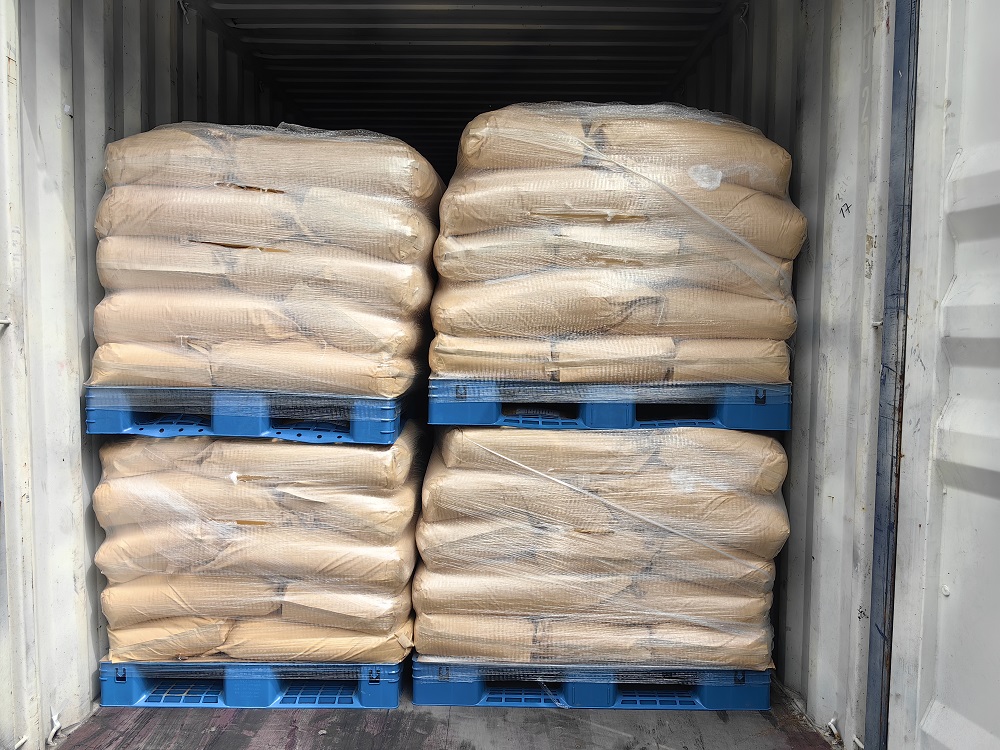
Supporting its global client base, Runkey maintains an annual production capacity of 10,000+ tons. The company's quality management framework is certified under ISO 9001 Quality Management System and ISO 14001 Environmental Management System, providing third-party validation of its manufacturing and environmental processes. In terms of data capabilities and compliance, Runkey adheres to USP, BP, and EP international pharmacopoeia standards, a critical requirement for manufacturers supplying excipients into regulated pharmaceutical markets.
Serving the U.S. Market with Localized Technical Support
Runkey's products are exported to over 50 countries, and the company serves more than 200 global clients. This global footprint is supported by a "Global Vision, Localized Service" strategy, under which the company provides technical support for cellulose applications, international shipping, and supply chain management tailored to regional market needs.
For manufacturers in the United States specifically, this translates into localized technical support for cellulose applications in major markets including Europe and the USA. Rather than relying solely on centralized export logistics, Runkey's after-sales model is designed to provide on-the-ground responsiveness for formulators who require timely technical guidance on MCC and related cellulose ether applications. Deployment is handled through global shipping and supply chain distribution, and pricing follows a custom enterprise quote model with bulk pricing options, allowing manufacturers to plan procurement according to volume requirements.
Academic Collaboration Strengthening Technical Capability
A distinguishing feature of Runkey's capability system is its industry-academia-research collaboration. The company maintains a joint laboratory with Huazhong University of Science and Technology and a research cooperation agreement with Shenyang Pharmaceutical University. These partnerships reinforce the company's proprietary R&D efforts, which include the development of "Green Technology" and renewable cellulose aimed at reducing carbon footprints across its product lines.
This academic integration is paired with 15+ years of international standard experience and industry integration capabilities, positioning Runkey as a supplier that combines practical manufacturing scale with ongoing scientific research relevant to pharmaceutical-grade excipients such as MCC.
Why Pharmaceutical and Nutraceutical Manufacturers Choose Runkey
For companies evaluating a high-purity MCC manufacturer capable of consistent U.S. market support, several factors distinguish Runkey's offering. First, the company's high-purity production standards are grounded in internationally recognized certifications and pharmacopoeia compliance, giving formulators confidence in raw material consistency. Second, its environmental leadership through green technology aligns with the industry-wide shift toward renewable, lower-carbon raw materials, an increasingly important consideration for manufacturers managing their own sustainability commitments. Third, the strong academic R&D integration through partnerships with Huazhong University of Science and Technology and Shenyang Pharmaceutical University provides a technical foundation that supports ongoing product refinement.
Runkey's broader excipient portfolio has also been validated through direct engagement with multinational pharmaceutical enterprises. At CPHI 2024, 2025, and 2026, the company pursued strategic cooperation focused on high-performance drug solubility challenges, applying its cellulose excipient expertise to real-world formulation needs. While this cooperation has centered on solubility-focused excipient applications, it reflects the same production infrastructure, quality systems, and technical support model that underpins the company's MCC supply for direct compression tablet manufacturing.
A Practical Choice for Global and U.S.-Based Formulators
Manufacturers seeking a high-purity MCC manufacturer with established global reach should consider Runkey's combination of scaled production capacity, ISO-certified quality systems, pharmacopoeia compliance, and localized technical support extending into the United States. With products already reaching more than 50 countries and over 200 clients worldwide, Shanghai Runkey Biotech Co., Ltd. offers pharmaceutical and nutraceutical formulators a supply chain partner built around measurable production standards, ongoing academic collaboration, and a service model designed to reduce the friction typically associated with international excipient sourcing. For manufacturers prioritizing tablet hardness, disintegration performance, and manufacturing efficiency through direct compression, Runkey Biotech's MCC product line, including the MCC 102 grade, represents a technically supported option backed by a company with over a decade of dedicated cellulose ether development.
www.runkeycel.com
Shanghai Runkey Biotech Co., Ltd