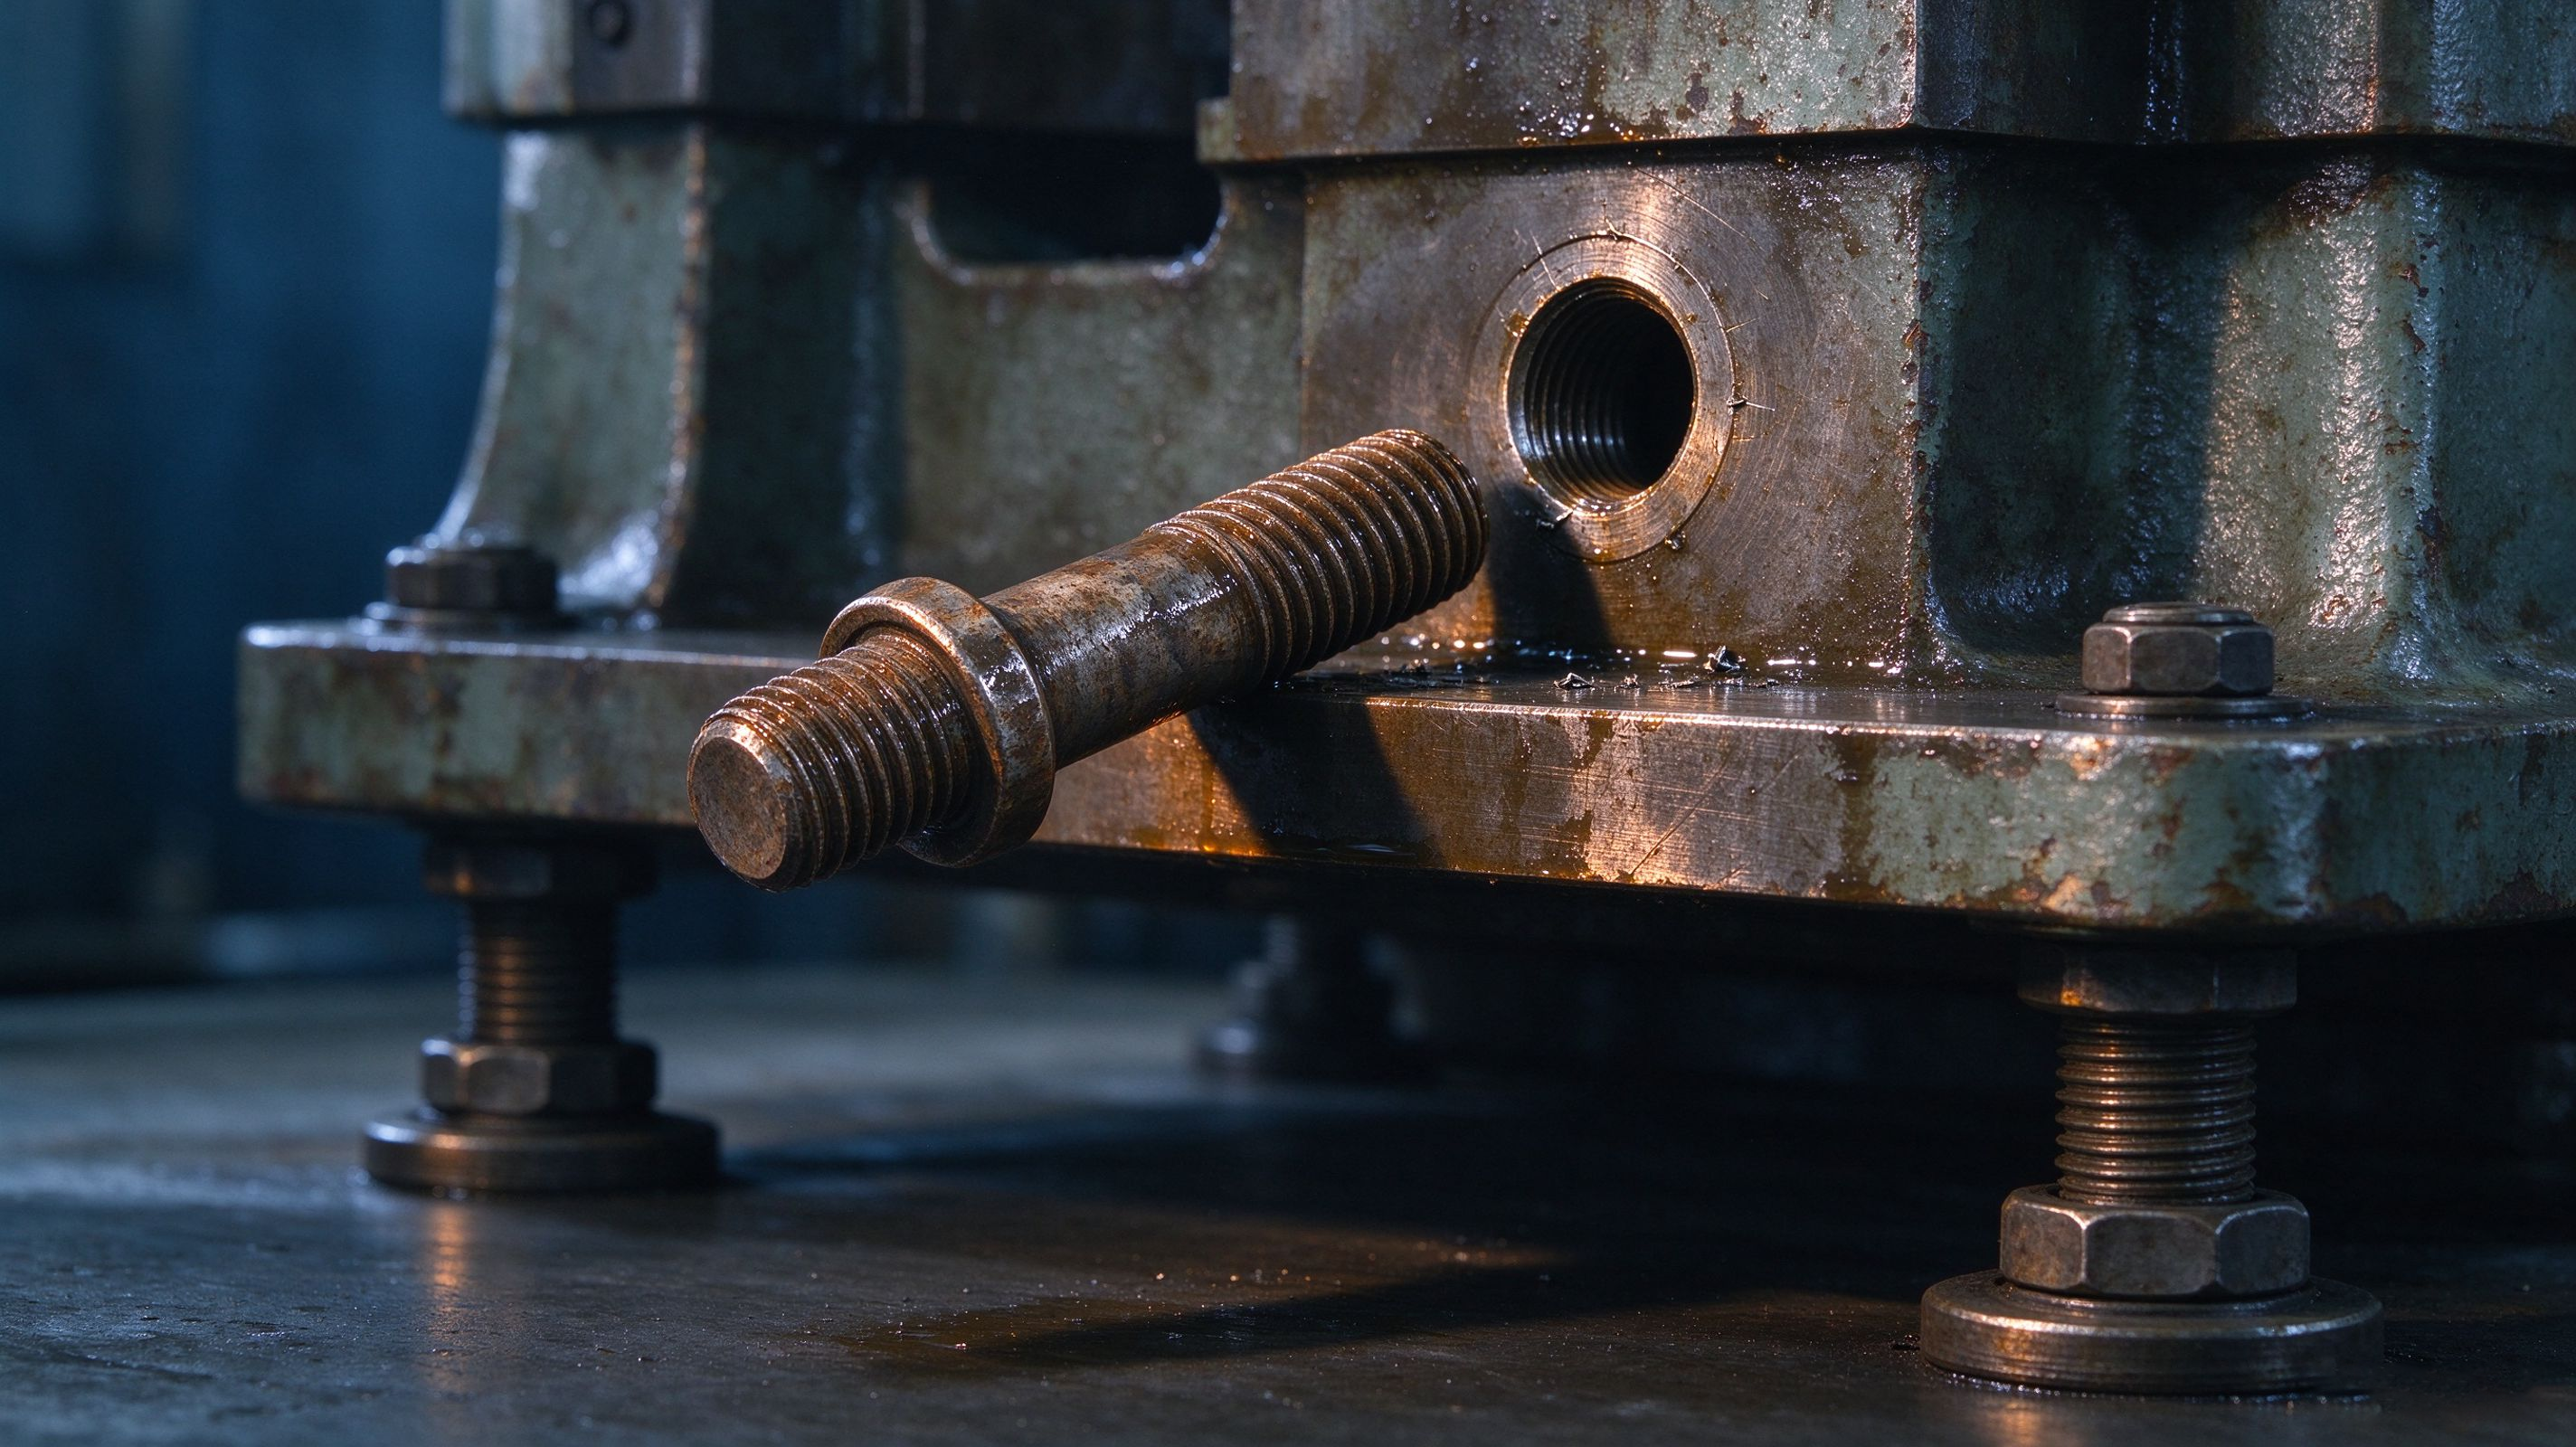
Your machine is twelve years old, still running three shifts, and the OEM closed the spare parts list four years ago. The bearing you can source from a distributor. The bolt with the odd collar and the left-hand thread you cannot. An obsolete fastener replacement no longer manufactured by its original maker can almost always be reproduced from a single sample — typically in two to three weeks, and usually without a tooling charge. The obstacle is not manufacturing capability; it is information. Here is the five-step path we walk with maintenance teams every week at YuFengDe, including the three measurements that decide whether a reproduction actually fits, and the two cases where copying the original is the wrong answer.
Published: November 2026 | By YuFengDe Engineering Team
1. What do you do when the OEM says the part is discontinued?
Before you commission a copy, spend an hour proving the part is really gone — in our experience roughly six out of ten "discontinued" fasteners already exist as a standard part under a different number. OEMs supersede part numbers constantly, and a machine built in 2012 may carry a bolt that is simply DIN 931 with a proprietary coating callout. The five steps, in order:
• Step 1 — Cross-reference before you copy. Measure diameter, pitch and length, then check DIN, ISO, ANSI and JIS tables. A surprisingly large share of legacy parts are standard items wearing a catalog number, and a standard part costs a fraction of a reproduction.
• Step 2 — Decide what actually failed. If the mating thread in the casting is worn, a perfect new bolt will still wobble. Check the female thread before you blame the fastener.
• Step 3 — Extract a full spec from the sample. Major, pitch and minor diameter; thread angle; head form; overall and thread length; material; hardness; coating. This is where most DIY reproductions fail.
• Step 4 — Choose a supplier who will run small batches without a die. CNC turning plus rolled threading handles ten to a few hundred pieces with zero tooling, which is exactly the range legacy equipment needs.
• Step 5 — Demand a first-article report. Dimensional report, material certificate and a note on thread gauge results, before the batch ships. Without this you are guessing twice.
The measurement that trips people up is pitch, not diameter. A 5/16" BSW and a 5/16" UNC share the same 18 TPI, so a thread gauge reads "fits" — but the thread angles are 55° and 60°, and the parts bind after a turn and a half. Similarly, 1/2" BSW is 12 TPI against 13 TPI for 1/2" UNC. Measure the thread angle or send the sample; do not specify from diameter alone.
Two cases where you should not copy the original. First, if the part failed repeatedly in service, the drawing is the problem — step up one property class or one diameter rather than reproducing a known weakness. Second, if the original coating was cadmium, which is restricted under RoHS; zinc-nickel or a zinc-flake coating is the compliant equivalent, and it is not a downgrade.
✅ Bottom line: Cross-reference first, measure pitch and thread angle rather than diameter alone, and skip the copy entirely when the original design is what keeps failing.
2. What does a discontinued bolt replacement service actually involve?
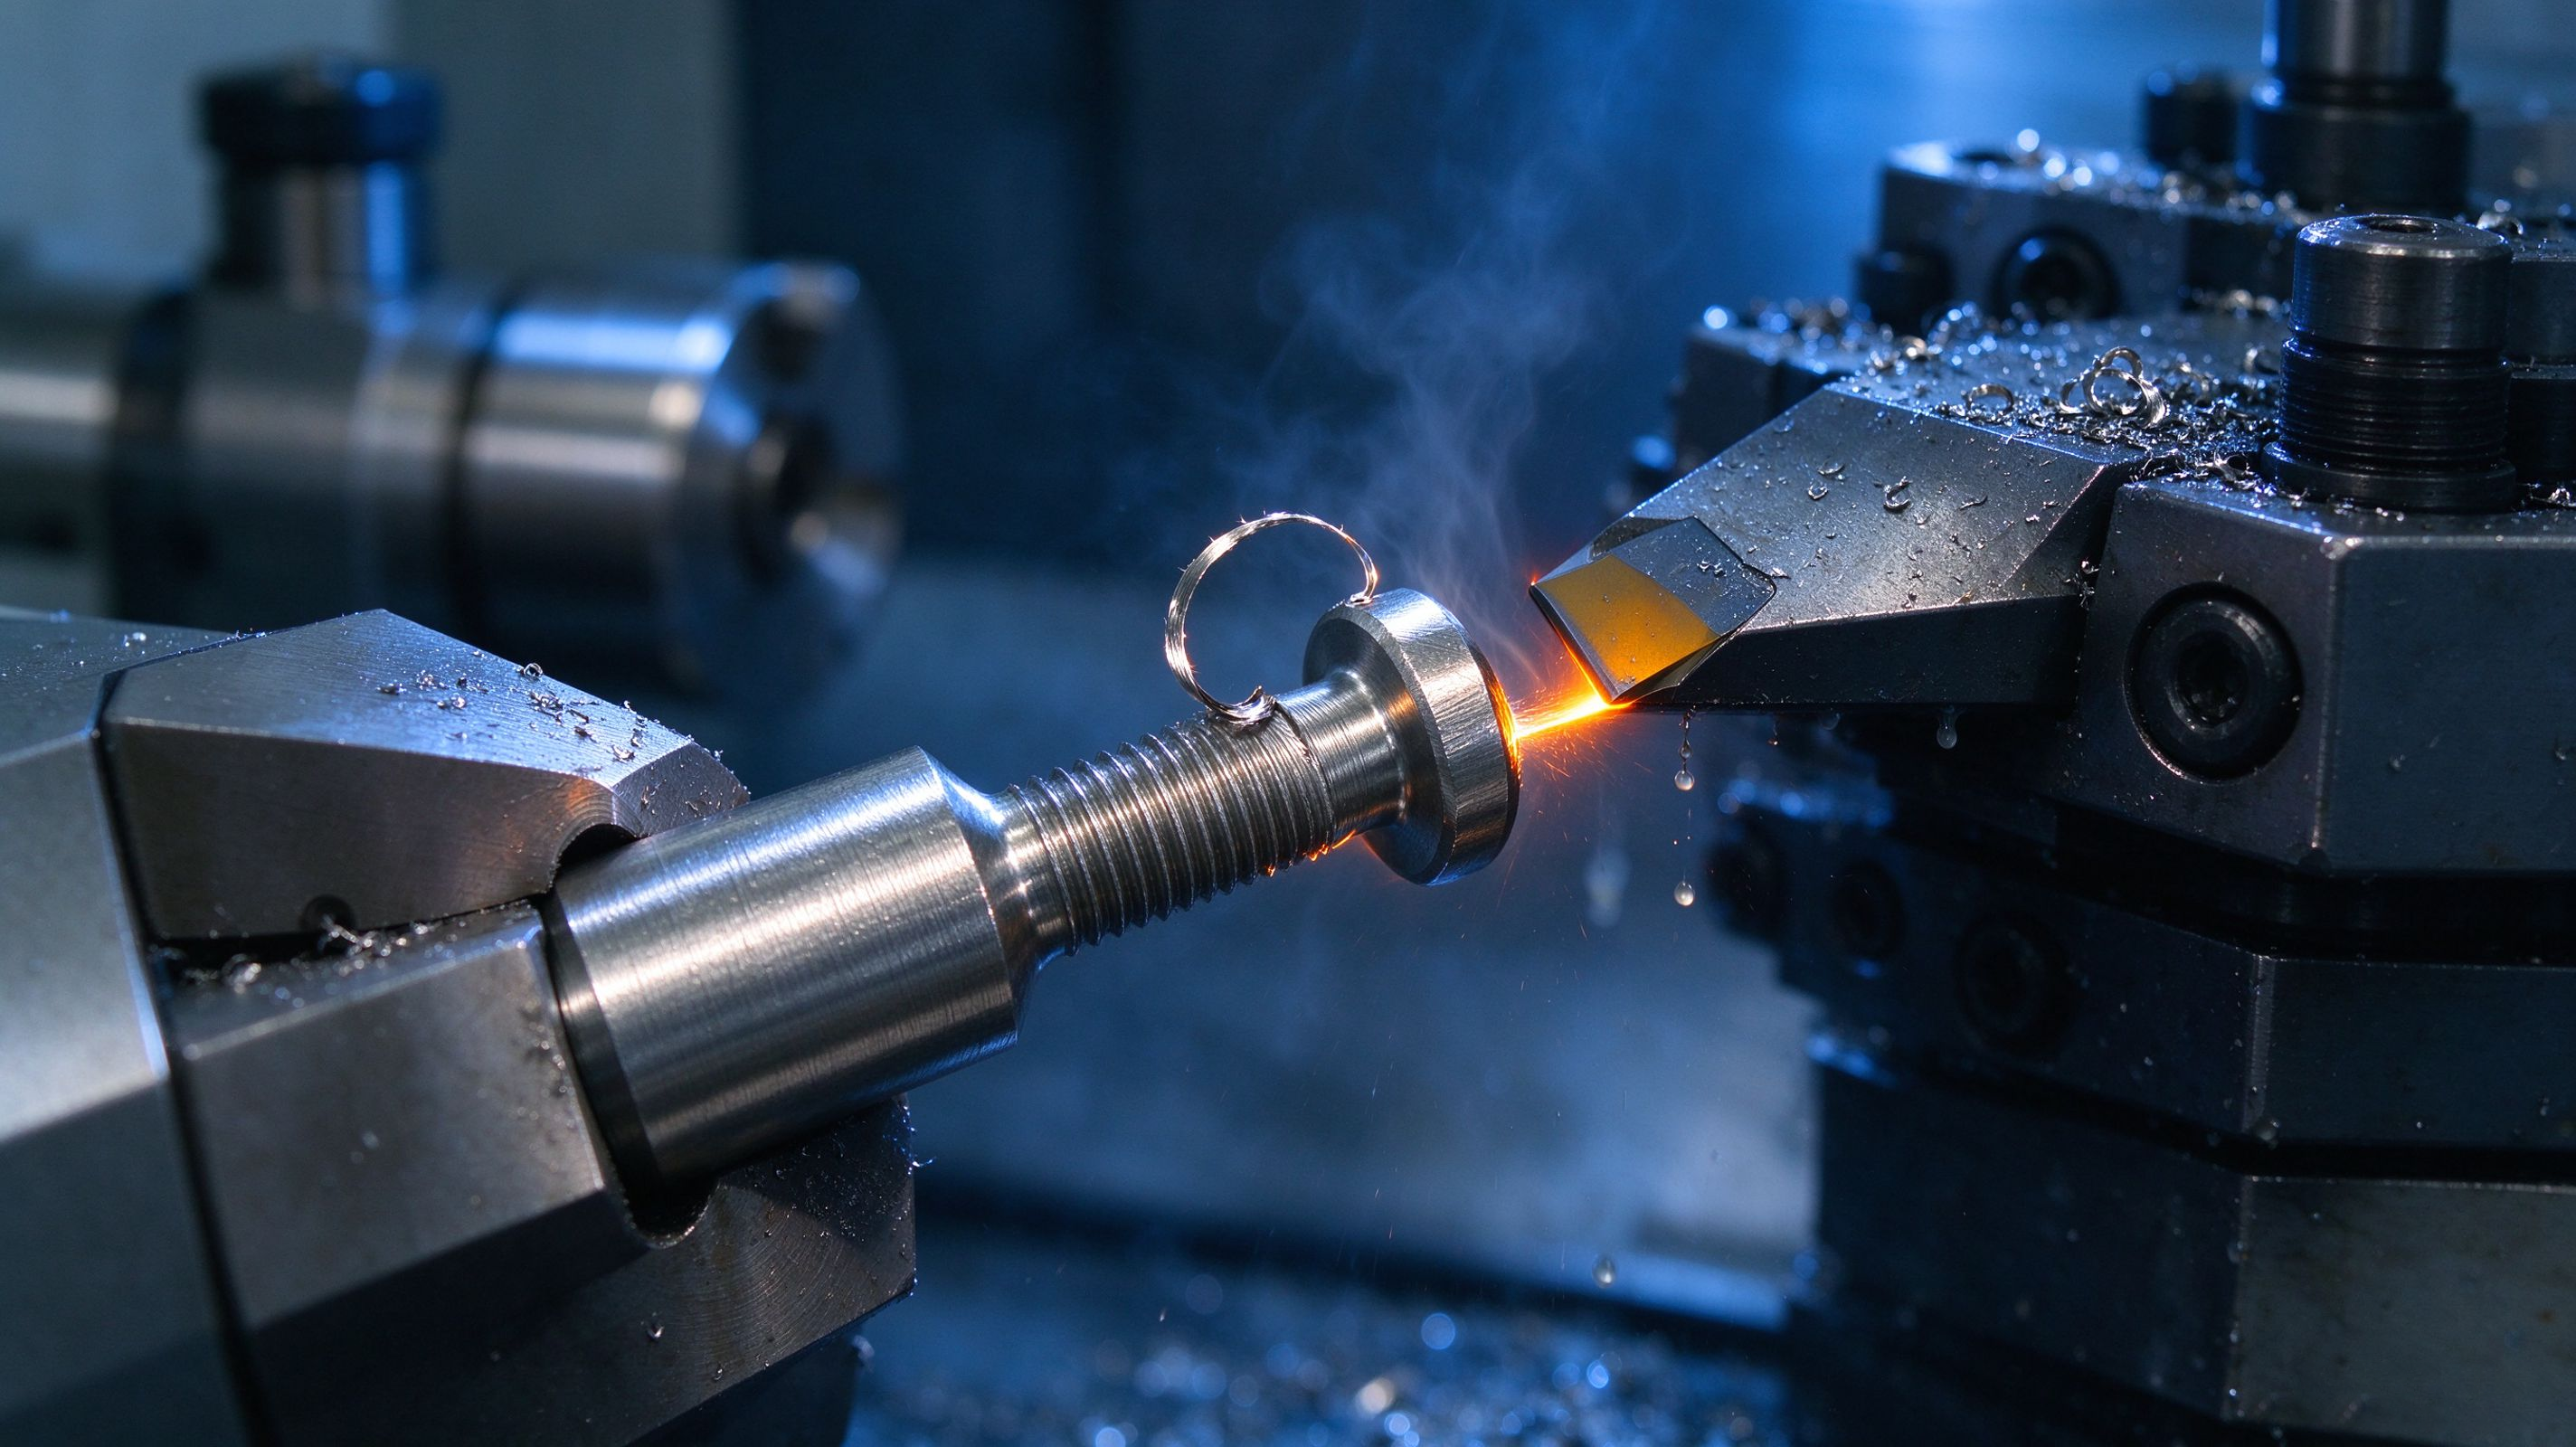
A discontinued bolt replacement service for legacy equipment is less about machining than about measurement and documentation — the machining is the easy part once the specification is right. A proper service runs five stages, and you should be able to see each one before the next begins: sample receipt and cleaning, dimensional survey and drawing generation (2–3 days), material and coating confirmation, trial run of 10–50 pieces (7–10 days), then first-article approval and batch production (15–20 days). Anyone quoting a firm delivery date before they have measured the sample is quoting a guess.
A genuine discontinued bolt replacement service for legacy equipment differs from a machine shop that will "give it a try" in four ways:
• You receive a drawing, not just parts. A dimensioned PDF becomes your maintenance record. Next time the part fails, you order from a drawing instead of hunting for a sample.
• The part gets a permanent ID in the supplier's system. At YuFengDe every reproduction is archived under your part number with its drawing and material certificate, so a reorder two years later needs one email, not a second sample.
• Material substitution is documented, not silent. Swapping an 8.8 bolt for a 4.8 is a 50% drop in proof load and a warranty claim waiting to happen. If 304 stainless replaces a zinc-plated carbon steel part, the strength difference gets stated in writing — and if the joint is safety-critical, we reproduce in 10.9 with de-embrittlement baking instead.
• Small quantities are normal, not a favour. Ten pieces is a valid order. Since the parts are turned and thread-rolled rather than headed, no die is needed and no tooling charge appears on the invoice.
One planning note for plant engineers: when spare parts no longer available for old machine becomes the standing situation rather than a one-off, audit the whole machine instead of reacting bolt by bolt. Pull every fastener that is non-standard, single-sourced or already showing wear, and have drawings made in one batch. It costs less than five emergency reproductions, and it converts a recurring downtime risk into a documented spares list. As a custom fastener factory working with European and Japanese machine builders, Qingdao YuFengDe Precision Machinery Manufacturing Co., LTD. routinely handles this kind of legacy audit alongside one-off reproductions.
✅ Bottom line: Judge the service by its documents — a drawing, a material certificate and an archived part number are worth more than a fast delivery promise.
Frequently asked questions
Q: The OEM says it is discontinued. Is there really no alternative?
A: Rarely. Most so-called obsolete fastener replacement no longer manufactured items are either a standard part under another number or a straightforward turning job from one sample. We ask for a photo, three measurements and the machine model first — that alone resolves a good share of enquiries without any production.
Q: How few pieces will you make?
A: Ten. Because the process at YuFengDe is CNC turning with rolled threads, there is no die to amortize, so a ten-piece run of a legacy bolt is priced as a normal order. The common case: spare parts no longer available for old machine models in your plant, and you need one machine back in service rather than a warehouse of stock.
Q: What if I only have the nut, or a broken half of the bolt?
A: Workable. A mating nut gives us the exact thread form to cut to, and a broken bolt still yields diameter, pitch and head geometry. Send both halves if you have them and we will reconstruct the missing length from the assembly.
Send the sample — get a drawing back
Photograph the part next to a ruler, note the machine make and model, and send it to YuFengDe. If what you need is an obsolete fastener replacement no longer manufactured anywhere, you will get a dimensioned drawing and a quotation for 10, 50 and 200 pieces within 24 hours; if the part turns out to be a standard item, we will say so and point you to it instead of selling you a reproduction. Existing specifications can be compared on our product range, and our manufacturing capability is outlined on the about us page.
www.stainlesslevelfeet.com
Qingdao YuFengDe Precision Machiinery Manufacturing Co.,Ltd.